


Engineered for Subsurface Performance
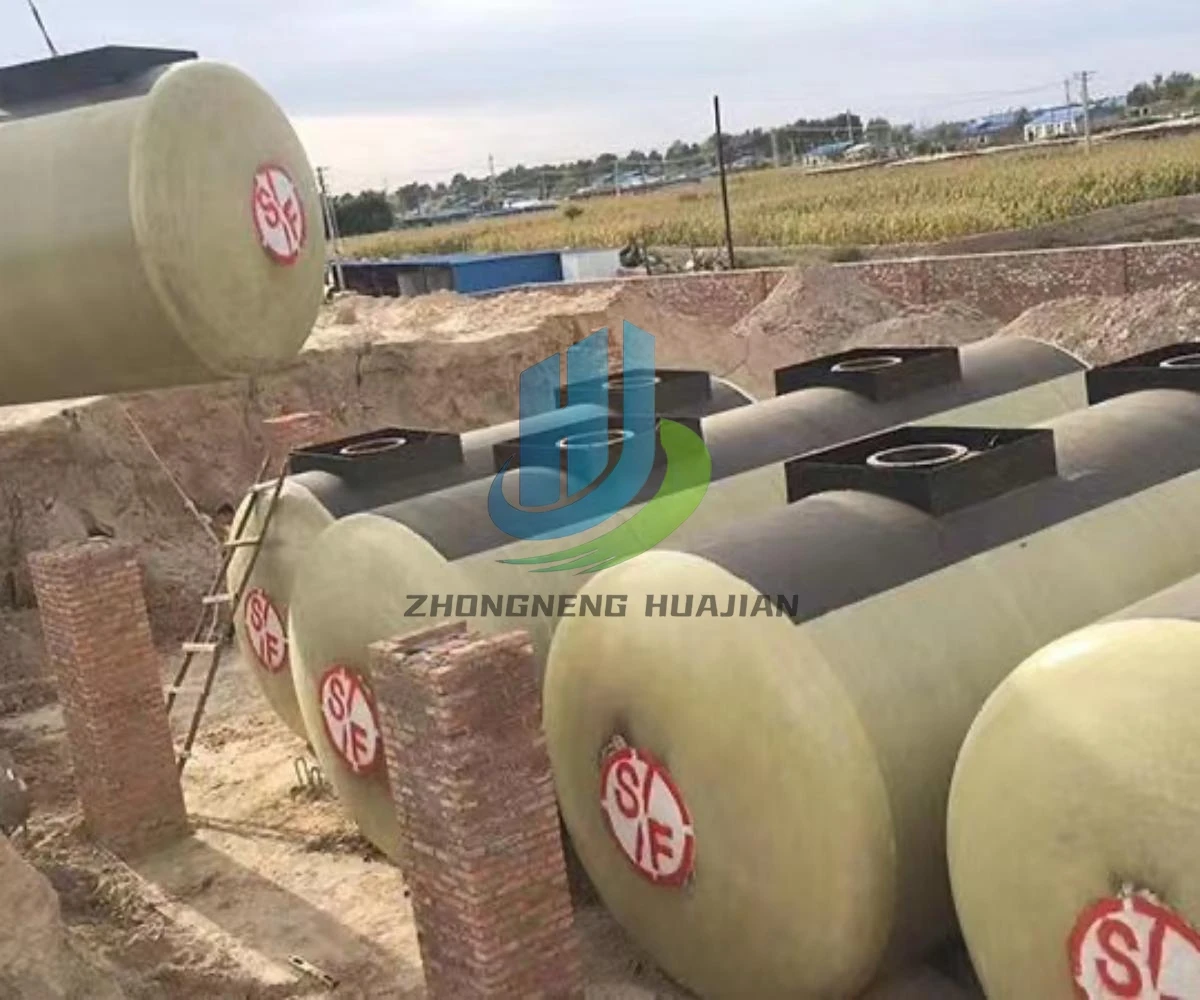
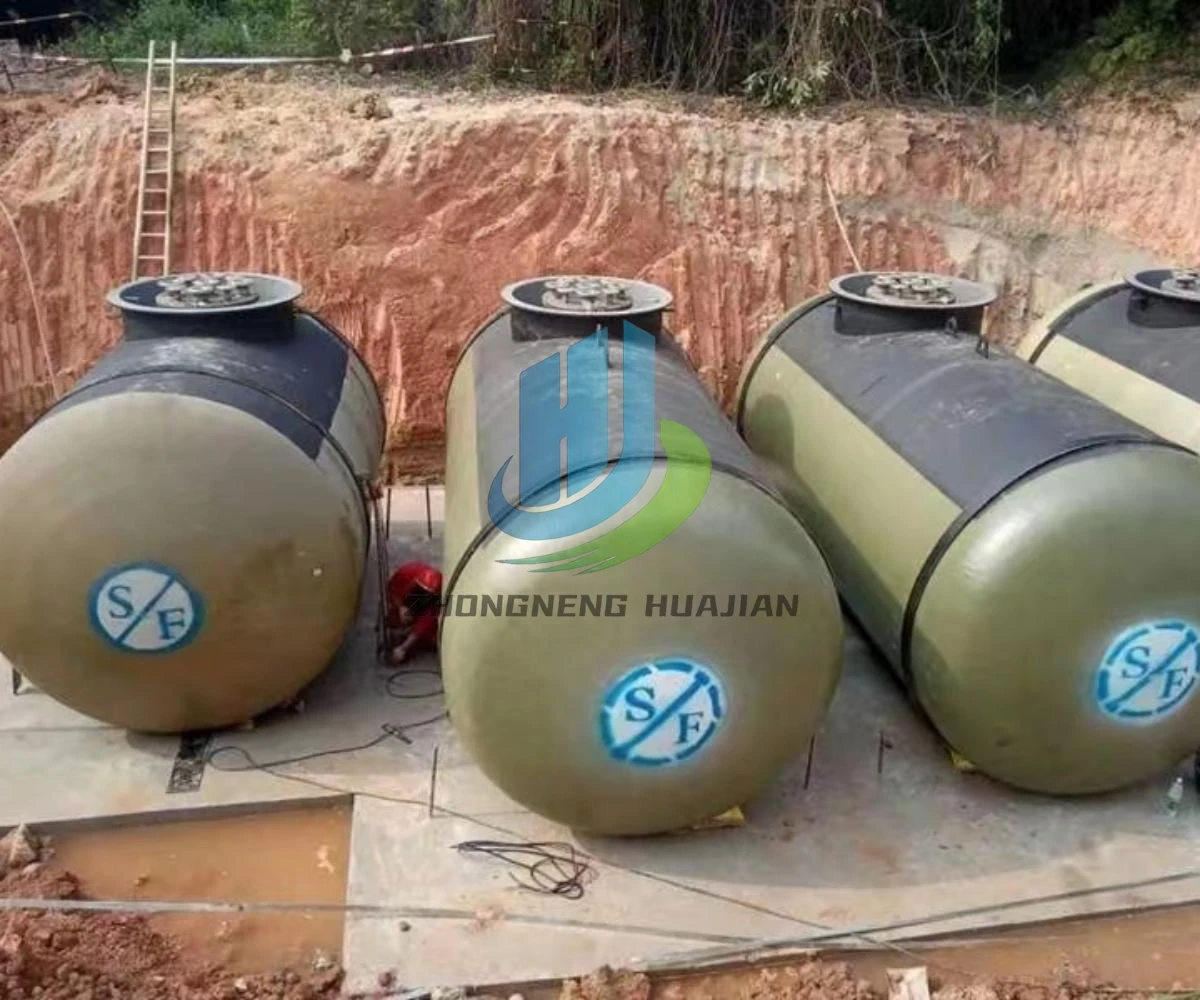
Designed to endure constant soil pressure and dynamic surface loads, our underground tanks feature:
- Reinforced Wall Construction: Enhanced thickness and structural design to withstand long-term burial stresses
- Dual-Phase Corrosion Protection: Combining high-performance coating systems with active cathodic protection
- Buoyancy Management: Integrated anchoring systems prevent displacement in high-water-table environments
Applications Across Industries
These versatile tanks serve critical functions in diverse sectors:
Fuel Management
Gasoline, diesel, and aviation fuel storage at service stations, airports, and transport depots
Chemical Processing
Secure containment of temperature-sensitive or regulated chemical products
Water Infrastructure
Potable water reserves, stormwater retention, and wastewater buffer capacity
Industrial Operations
Process liquid storage requiring stable conditions and space optimization
Integrated Safety and Monitoring Systems
Every installation incorporates comprehensive safety engineering:
• Leak Detection Networks: Monitoring wells and electronic sensors for continuous environmental protection
• Engineered Backfill Systems: Specially graded materials and compaction protocols to ensure uniform support
• Access and Ventilation: Strategically positioned manways, vents, and inspection ports for maintenance accessibility
• Secondary Containment: Optional double-wall construction or liner systems for enhanced environmental protection
Professional Implementation Process
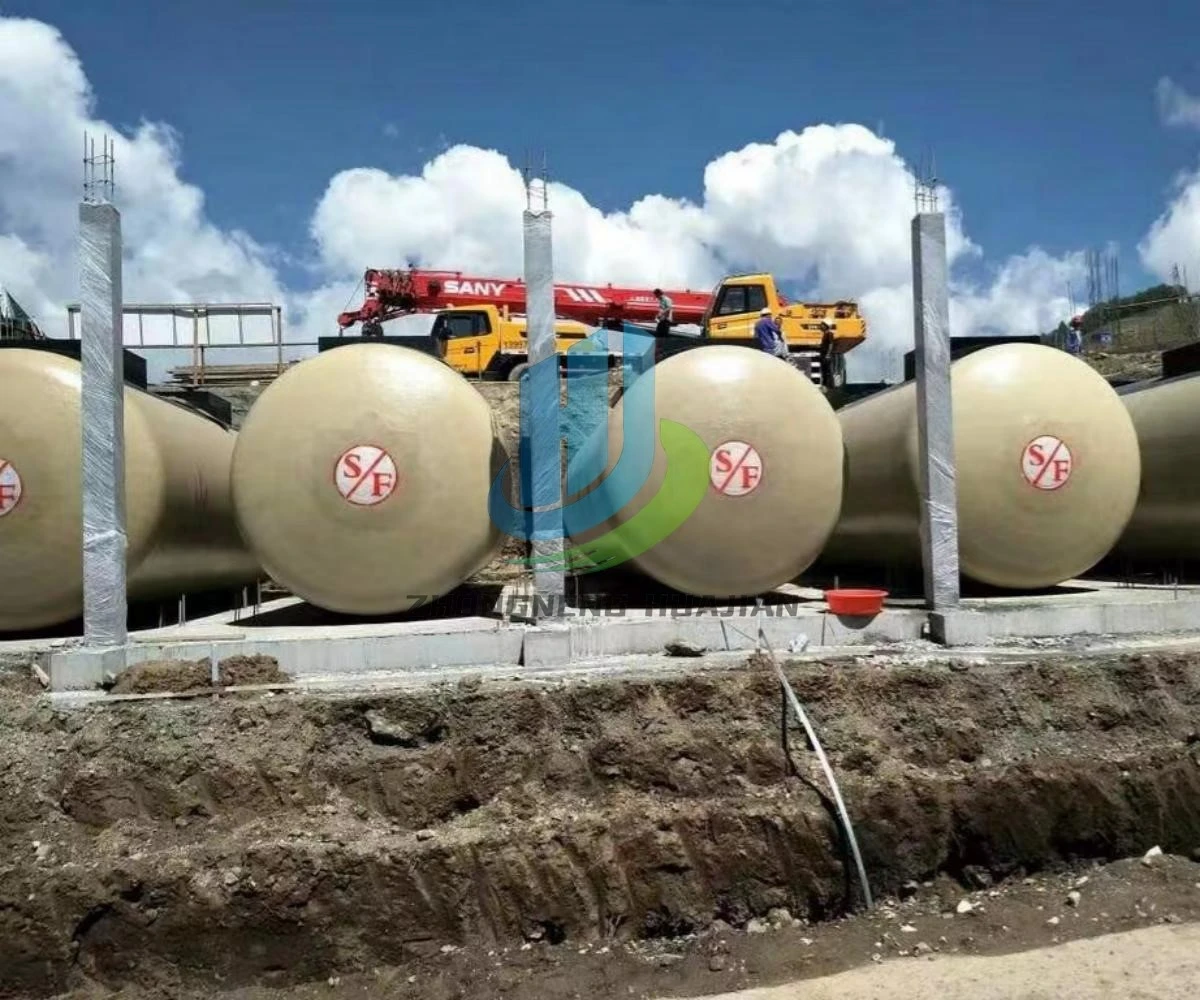
Our turnkey approach ensures proper installation and long-term reliability:
1. Site Evaluation: Geological assessment and regulatory compliance review
2. System Engineering: Custom design including structural calculations and corrosion protection specification
3. Precision Installation: Controlled placement, anchoring, and backfilling by certified technicians
4. Commissioning and Validation: Comprehensive testing, monitoring system activation, and documentation
5. Ongoing Support: Maintenance protocols, inspection services, and regulatory compliance assistance
Technical Advantages of Our Underground Systems
Space Optimization: Maximize usable surface area while maintaining full storage capacity
Thermal Regulation: Natural ground insulation minimizes temperature fluctuations
Environmental Security: Multiple barrier protection against soil and groundwater contamination
Longevity: Advanced materials and protection systems extend service life beyond conventional expectations
Regulatory Alignment: Engineered to meet or exceed international standards including API, UL, and local environmental regulations
Beyond Basic Storage: A Managed Solution
Our underground tanks represent more than simple containment vessels-they are integrated storage systems complete with monitoring technology, safety features, and professional implementation services. This comprehensive approach transforms underground storage from a basic necessity into a managed asset that supports operational efficiency, regulatory compliance, and environmental responsibility. For organizations seeking intelligent storage solutions that balance capacity, security, and space utilization, our horizontal underground tank systems provide a technically advanced foundation for liquid management infrastructure.
Hot Tags: horizontal underground storage tanks, China horizontal underground storage tanks manufacturers, suppliers, Horizontal Double walled Oil Tank, Fiberglass Horizontal Storage Tank, Stainless Steel Horizontal Storage Tank, horizontal storage tank, Horizontal Above ground Oil Tank, Horizontal Underground Storage Tanks


