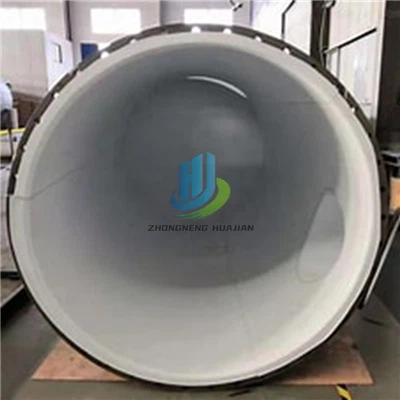
Engineered for Maximum Thermal Retention & Durability
Constructed from robust carbon steel, the tank's core is integrated with a high-performance internal coil heating system. We offer flexible configurations for thermal oil, steam, or electric heat sources to seamlessly match your site's existing utilities. The critical insulation barrier utilizes high-density rock wool, with thickness scientifically calibrated to your specific climatic conditions, guaranteeing minimal temperature drop. This is all protected by a durable, profiled color steel sheet outer cladding, which shields the insulation from environmental damage and ensures long-term structural integrity. Every component is designed to achieve the perfect equilibrium between unparalleled thermal retention and rugged, practical operation.
Streamlined Automation & Tangible Operational Advantages
The operation is designed for simplicity and reliability. Asphalt is loaded via the top, and from there, the intelligent automated system takes over. It maintains precise temperature control within preset parameters, eliminating guesswork. Integrated temperature sensors enable smart interlock controls that proactively prevent both overheating-which can cause premature aging and degradation of the asphalt-and under-heating, which risks solidification. The advantages are clear and impactful:
Quality Preservation
Protects the original asphalt specifications by maintaining a stable temperature window, eliminating thermal degradation.
Enhanced Efficiency & Reduced Costs
Fully automated process control minimizes labor requirements and the potential for human error, lowering operational overhead.
Optimal Space Utilization
The vertical design offers a minimal footprint, a critical advantage for space-constrained asphalt plants or congested project sites.
Uninterrupted Workflow
Ensures a reliable, on-demand supply of ready-to-use paving material, keeping your projects on schedule.
Proactive Safety, Sustained Performance & Full-Cycle Support
Safety and long-term durability are foundational to our design. The system is equipped with comprehensive safeguards, including over-temperature alarms, pressure relief valves, and certified monitoring instrumentation. To safeguard your investment and maintain peak efficiency, we recommend a simple, routine maintenance protocol. We further support you with complete operational training and detailed maintenance guidance-such as inspecting heating coils for coke formation-ensuring your asphalt storage tank delivers long-term, stable performance and a superior return on investment, year after year.
Hot Tags: vertical asphalt storage tank, China vertical asphalt storage tank manufacturers, suppliers, Stainless Steel Vertical Storage Tank, Vertical Asphalt Storage Tank, vertical storage tank, Vertical Fly Ash Storage Tank, Vertical Steel lined PTFE Storage Tank, vertical mobile tank system