


Product Features
1. Superior Durability: Constructed with premium-grade steel or food-grade polyethylene, resistant to rust, UV rays, and chemical corrosion.
2. High Capacity Efficiency: 500-ton storage volume optimized for space-saving installation without compromising structural stability.
3. Easy Maintenance: Smooth inner surface prevents sediment buildup; leak-proof design reduces long-term upkeep costs.
4. Versatile Installation: Suitable for above-ground and semi-underground setups, adaptable to diverse site conditions.
5. Safety Certified: Complies with international storage standards, equipped with overflow and drainage systems for risk prevention.
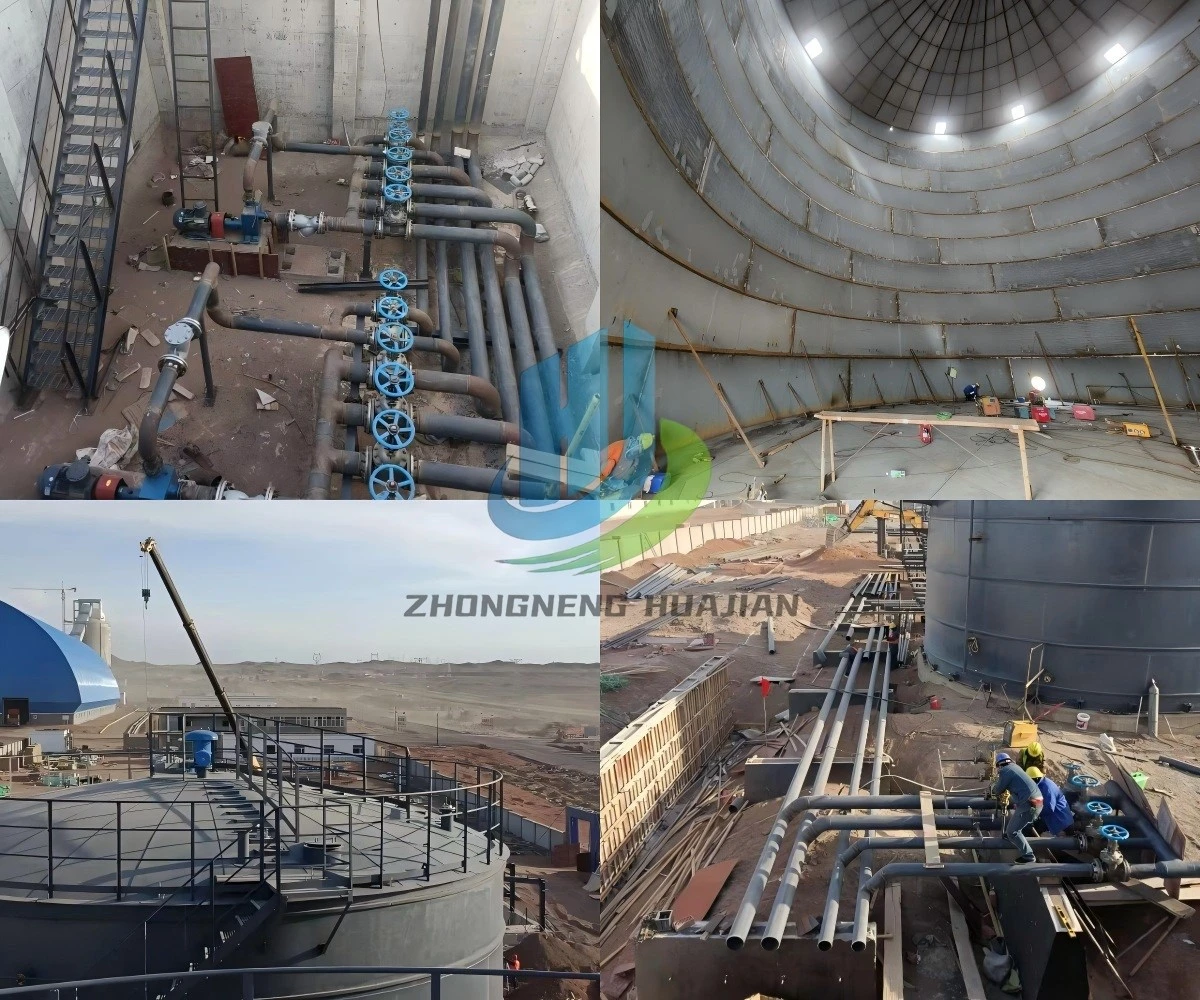
Technical Parameters
| Parameter | Specification |
| Storage Capacity | 500 tons (500,000 liters) |
| Material | Q235B carbon steel / Food-grade HDPE |
| Dimensions | Customizable (standard: 15m×8m×4.5m) |
| Working Temperature | -20℃ to 60℃ |
| Pressure Rating | Atmospheric pressure |
| Certification | ISO 9001, CE |
Craft Technology
The 500-ton water tank adopts a seamless welding process for steel models, ensuring uniform stress distribution and zero leakage. For HDPE tanks, we use rotational molding technology to create a one-piece structure with no joints, enhancing impact resistance. All tanks undergo sandblasting and anti-corrosion coating treatment to extend service life. Precision cutting and CNC machining guarantee dimensional accuracy, while strict quality checks are implemented at every production stage.
Application Scenarios
Agricultural Irrigation:
Store large volumes of water for farmland irrigation in arid or water-scarce regions.
Industrial Use:
Hold process water, cooling water, or wastewater for manufacturing plants, construction sites, and mining operations.
Municipal Water Supply:
Supplement urban water storage systems to meet peak demand or emergency water needs.
Rainwater Harvesting:
Collect and store rainwater for sustainable use in landscaping, toilet flushing, and fire fighting.
FAQ
Hot Tags: 500-ton water tank, China 500-ton water tank manufacturers, suppliers, Large Fire Fighting Water Tank, Vertical Fire Water Tank, Vertical Water Storage Tank, Stainless Steel Fire Water Tank, Fire Fighting Water Storage Tank, 500 ton Water Tank


